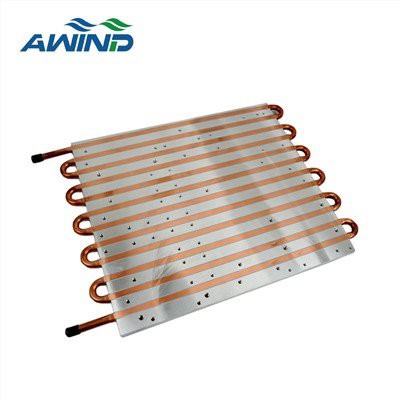
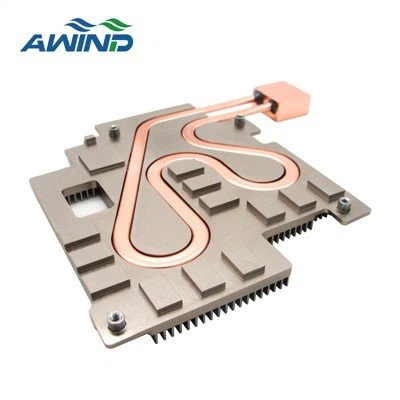
We focus on the management and risk control of each link in the industry chain to achieve full product traceability and ensure the quality of Heat Sink with Copper Heat Pipe, OEM Heat Sink, Vacuum Brazing Liquid Cooling Heatsink. The company always adheres to the customer first service attitude, develops together with new and old customers on the premise of mutual benefit, and sincerely establishes good cooperative relations with all customers. We have been actively participating in professional academic activities in related fields and organizing various domestic and international academic exchanges to promote the overall academic development of the professional field. Our products have been widely praised after being put into the market, with high customer satisfaction and reputation.
Brazing
Brazing is the jointing of metals using a molten filler material, which on cooling forms a joint.
The filler metal melting temperature is above 450℃, but below the melting point of the metals.
How does it work?
Brazing joints the base metals by creating a metallurgical bond between the filler metal and the base metals.
When molten, the filler metal is drawn into the joint by capillary action.

How do you supply filler metal to 100's of joint simultaneously?
Brazing sheet!

Aluminum oxide
Aluminum oxide characteristics:
Hardness significantly above 400Mpa
High resistance to chemicals
The oxide interferes with brazing
Aluminum owes many of its properties to very strong adherent oxide film on the surface.
This oxide must be removed or broken up if joining is to occur.
There are a number of possibilities of achieving this.

Comparison of brazing processes:
CAB | Vacuum brazing | Air furnace brazing | |
Heating | Radiation/Convection | Radiation | Forced convection |
Use of flux | Yes | NO | NO |
Quantity of flux | <5g/㎡ | - | 30~50g/m³ |
Pre braze treatment | Moderate demands | High demands | Moderate demands |
Post braze treatment | NO | NO | Yes |
Aqueous wastes | NO | Yes | |
Atmospheric emissions | NO | NO | NO |
Continuos process | Yes | NO | Yes |
Investment | 80 | 100 | 90 |
Operating expense | 80 | 100 | 100 |
CAB furnace brazing process sequence
The CAB process sequence is depending on: Heat exchanger design, Cleaning method, Flux application method.

CAB furnace braze cycle

Factors determining CAB production success or failure
1. Good product fit-up ( gap tolerance 0.1 to 0.15mm)
2. Adequate quantity of filler metal
3. Uniformity of flux coating
4. Interaction of flux and alloying elements
5. Furnace conditions (temperature time profile, temperature uniformity, furnace atmosphere)

We attach great importance to the cost price and profit opportunity of our Air Cooled Plate and Bar Aluminum Radiator Cores for Oil Cool Core and Intercooler, which can provide the basis for the scientific decision of our leaders. Adhering to the tenet of faithful, professional and enthusiastic service, we will expand more sales channels, expand market share and grasp potential business opportunities. We shoulder the mission of 'making employees happy, achieving customers and benefiting the society'.
Hot Tags: Vacuum Brazing Process, China, suppliers, manufacturers, factory, customized, free sample, made in China, Aluminum Extrusion Profiles Heat Sink, High Quality Cooling Heat Sink, Anodized Heatsink, Vacuum Brazing Liquid Cooling Heatsink, Bonded Fin Heat Sinks Assemblies, Industrial Water Cooling Cold Plate
[[ProKeywords]]