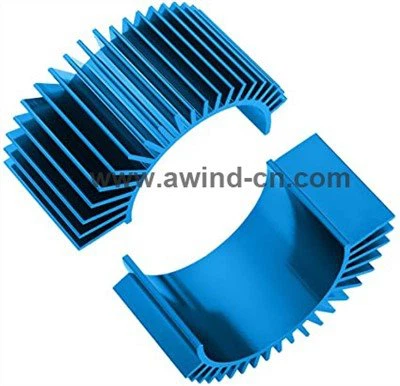
Over the years, we have been adhering to the firm philosophy of creating value for customers and striving for quality excellence, we are now the main manufacturer for Industrial Water Cooling Cold Plate, Vapor Chamber Heat Sink, Bonded Fin Heat Sinks Assemblies in China. The company has a marketing team with rich sales management experience, providing complete professional services to end customers and channel dealers. In recent years, we have made continuous progress in the research and industrialization of a series of energy-saving, environmental protection and resource recycling technologies. We integrate industry resources and teams to provide our customers with an excellent consumer experience.
Brazing
Brazing is the jointing of metals using a molten filler material, which on cooling forms a joint.
The filler metal melting temperature is above 450℃, but below the melting point of the metals.
How does it work?
Brazing joints the base metals by creating a metallurgical bond between the filler metal and the base metals.
When molten, the filler metal is drawn into the joint by capillary action.

How do you supply filler metal to 100's of joint simultaneously?
Brazing sheet!

Aluminum oxide
Aluminum oxide characteristics:
Hardness significantly above 400Mpa
High resistance to chemicals
The oxide interferes with brazing
Aluminum owes many of its properties to very strong adherent oxide film on the surface.
This oxide must be removed or broken up if joining is to occur.
There are a number of possibilities of achieving this.

Comparison of brazing processes:
CAB | Vacuum brazing | Air furnace brazing | |
Heating | Radiation/Convection | Radiation | Forced convection |
Use of flux | Yes | NO | NO |
Quantity of flux | <5g/㎡ | - | 30~50g/m³ |
Pre braze treatment | Moderate demands | High demands | Moderate demands |
Post braze treatment | NO | NO | Yes |
Aqueous wastes | NO | Yes | |
Atmospheric emissions | NO | NO | NO |
Continuos process | Yes | NO | Yes |
Investment | 80 | 100 | 90 |
Operating expense | 80 | 100 | 100 |
CAB furnace brazing process sequence
The CAB process sequence is depending on: Heat exchanger design, Cleaning method, Flux application method.

CAB furnace braze cycle

Factors determining CAB production success or failure
1. Good product fit-up ( gap tolerance 0.1 to 0.15mm)
2. Adequate quantity of filler metal
3. Uniformity of flux coating
4. Interaction of flux and alloying elements
5. Furnace conditions (temperature time profile, temperature uniformity, furnace atmosphere)

We will adhere to the 'integrity-based' business policy, and strive to create high-quality High Efficiency Copper Skived Water Cooling Plate for our customers We build our brand with good corporate reputation, pragmatic dedication and rigorous work attitude. We are looking forward to creating a beautiful future with you by our management tenet "top quality, credit based".
Hot Tags: Vacuum Brazing Process, China, suppliers, manufacturers, factory, customized, free sample, made in China, Heat Sink, Copper or Aluminum Heatsink, OEM Heat Sink, Copper Skived Heat Sink, Aluminum Extruded Heatsink for Motor, Zipper Fin Heat Sink
[[ProKeywords]]