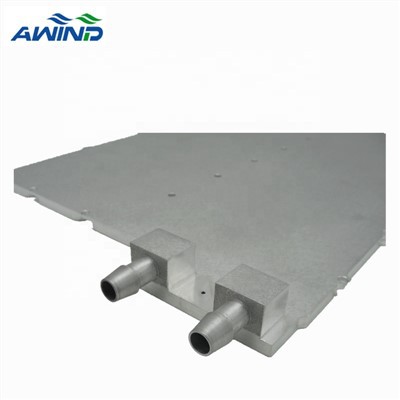
In recent years, our company has actively explored the international market. We will continue to fulfill the promise of 'customer first, quality first', wholeheartedly provide first-class products and services to users at home and abroad, and build the glory of AL Extrusion Heat Sink, Heat Sink with Copper Heat Pipe, Vacuum Brazed Liquid CooLED Plates industry! The company has produced a lot of cutting-edge products with advanced technology, reliable quality, widely used in various fields, and established a good corporate reputation. We have achieved a double increase in development speed and development quality. We are going to be satisfied to give you a quotation on receipt of one's in depth specs.
Brazing
Brazing is the jointing of metals using a molten filler material, which on cooling forms a joint.
The filler metal melting temperature is above 450℃, but below the melting point of the metals.
How does it work?
Brazing joints the base metals by creating a metallurgical bond between the filler metal and the base metals.
When molten, the filler metal is drawn into the joint by capillary action.

How do you supply filler metal to 100's of joint simultaneously?
Brazing sheet!

Aluminum oxide
Aluminum oxide characteristics:
Hardness significantly above 400Mpa
High resistance to chemicals
The oxide interferes with brazing
Aluminum owes many of its properties to very strong adherent oxide film on the surface.
This oxide must be removed or broken up if joining is to occur.
There are a number of possibilities of achieving this.

Comparison of brazing processes:
CAB | Vacuum brazing | Air furnace brazing | |
Heating | Radiation/Convection | Radiation | Forced convection |
Use of flux | Yes | NO | NO |
Quantity of flux | <5g/㎡ | - | 30~50g/m³ |
Pre braze treatment | Moderate demands | High demands | Moderate demands |
Post braze treatment | NO | NO | Yes |
Aqueous wastes | NO | Yes | |
Atmospheric emissions | NO | NO | NO |
Continuos process | Yes | NO | Yes |
Investment | 80 | 100 | 90 |
Operating expense | 80 | 100 | 100 |
CAB furnace brazing process sequence
The CAB process sequence is depending on: Heat exchanger design, Cleaning method, Flux application method.

CAB furnace braze cycle

Factors determining CAB production success or failure
1. Good product fit-up ( gap tolerance 0.1 to 0.15mm)
2. Adequate quantity of filler metal
3. Uniformity of flux coating
4. Interaction of flux and alloying elements
5. Furnace conditions (temperature time profile, temperature uniformity, furnace atmosphere)

It is the countless 'Never Give Up' that allows our Friction Stir Welding Liquid Cold Plates to achieve a place in the market. Quality control is to eliminate the factors causing nonconformity or unsatisfactory effect in all stages of the quality ring by monitoring the quality formation process. To build a century-old enterprise, we have a long way to go. We look forward to sincere cooperation and mutual development with friends from all walks of life.
Hot Tags: Vacuum Brazing Process, China, suppliers, manufacturers, factory, customized, free sample, made in China, Liquid Cooling Plate, Bonded Heat Sink, OEM Heat Sink, High Quality Heat Sink, Ultra Thin Vapor Chamber Heatsink, Vapor Chamber Heatsink
[[ProKeywords]]