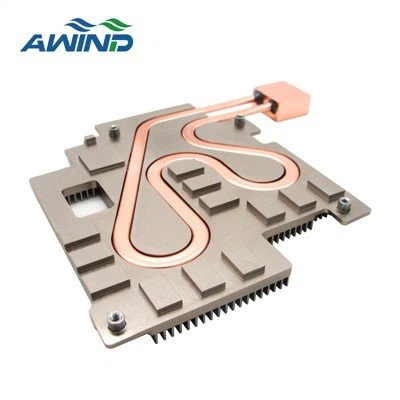
We are well aware that technology must be continuously improved, otherwise our CPU Heat Sink Design, Anodized Heatsink, Copper Skived Heat Sink will not be able to compete with other similar products. With our advanced technology advantages and superior product quality, we are now a world-renowned company. Our goal is to achieve the simultaneous realization of company value and personal value. The company uses precise targeted advertising to improve advertising and marketing effects, and uses a variety of innovative methods to maximize benefits. Our company is accelerating the transformation of economic development mode, promoting the construction of circular economy and forming the development mode of comprehensive development and utilization of resources and energy.
Brazing
Brazing is the jointing of metals using a molten filler material, which on cooling forms a joint.
The filler metal melting temperature is above 450℃, but below the melting point of the metals.
How does it work?
Brazing joints the base metals by creating a metallurgical bond between the filler metal and the base metals.
When molten, the filler metal is drawn into the joint by capillary action.

How do you supply filler metal to 100's of joint simultaneously?
Brazing sheet!

Aluminum oxide
Aluminum oxide characteristics:
Hardness significantly above 400Mpa
High resistance to chemicals
The oxide interferes with brazing
Aluminum owes many of its properties to very strong adherent oxide film on the surface.
This oxide must be removed or broken up if joining is to occur.
There are a number of possibilities of achieving this.

Comparison of brazing processes:
CAB | Vacuum brazing | Air furnace brazing | |
Heating | Radiation/Convection | Radiation | Forced convection |
Use of flux | Yes | NO | NO |
Quantity of flux | <5g/㎡ | - | 30~50g/m³ |
Pre braze treatment | Moderate demands | High demands | Moderate demands |
Post braze treatment | NO | NO | Yes |
Aqueous wastes | NO | Yes | |
Atmospheric emissions | NO | NO | NO |
Continuos process | Yes | NO | Yes |
Investment | 80 | 100 | 90 |
Operating expense | 80 | 100 | 100 |
CAB furnace brazing process sequence
The CAB process sequence is depending on: Heat exchanger design, Cleaning method, Flux application method.

CAB furnace braze cycle

Factors determining CAB production success or failure
1. Good product fit-up ( gap tolerance 0.1 to 0.15mm)
2. Adequate quantity of filler metal
3. Uniformity of flux coating
4. Interaction of flux and alloying elements
5. Furnace conditions (temperature time profile, temperature uniformity, furnace atmosphere)

The organization keeps for Best Quality Jx-012 Copper Brazed Water to Water Brazed Plate Heat Exchanger. We vigorously cultivate the innovation system, improve the incentive mechanism, restraint mechanism and fault tolerance mechanism, and create an open and inclusive atmosphere. On the basis of adopting advanced technology, our company pays close attention to the development direction of science and technology in the industry, improves the technology and product quality in time, and has won the trust and support of many customers.
Hot Tags: Vacuum Brazing Process, China, suppliers, manufacturers, factory, customized, free sample, made in China, Zipper Fin Heat Sink, Round Aluminum Heatsink for LED, Liquid Cold Plate, Heat Pipe Heat Sink, Aluminum Extrusion Profiles Heat Sink, Vc Heat Sink
[[ProKeywords]]